Production capabilities

From metal processing to large-scale steel structures.

Explore Production

Modern production facilities, advanced manufacturing technologies and qualified personnel allow SIVERGUMA to deliver complete metalworking solutions.

Production details

Our capabilities cover the key stages required to manufacture individual steel components, industrial tanks, autonomous field systems and large-scale structures for government, commercial and custom engineering projects.

Every production route is defined around the product: its geometry, material, operating environment, required accuracy, protective treatment, documentation and final delivery conditions.

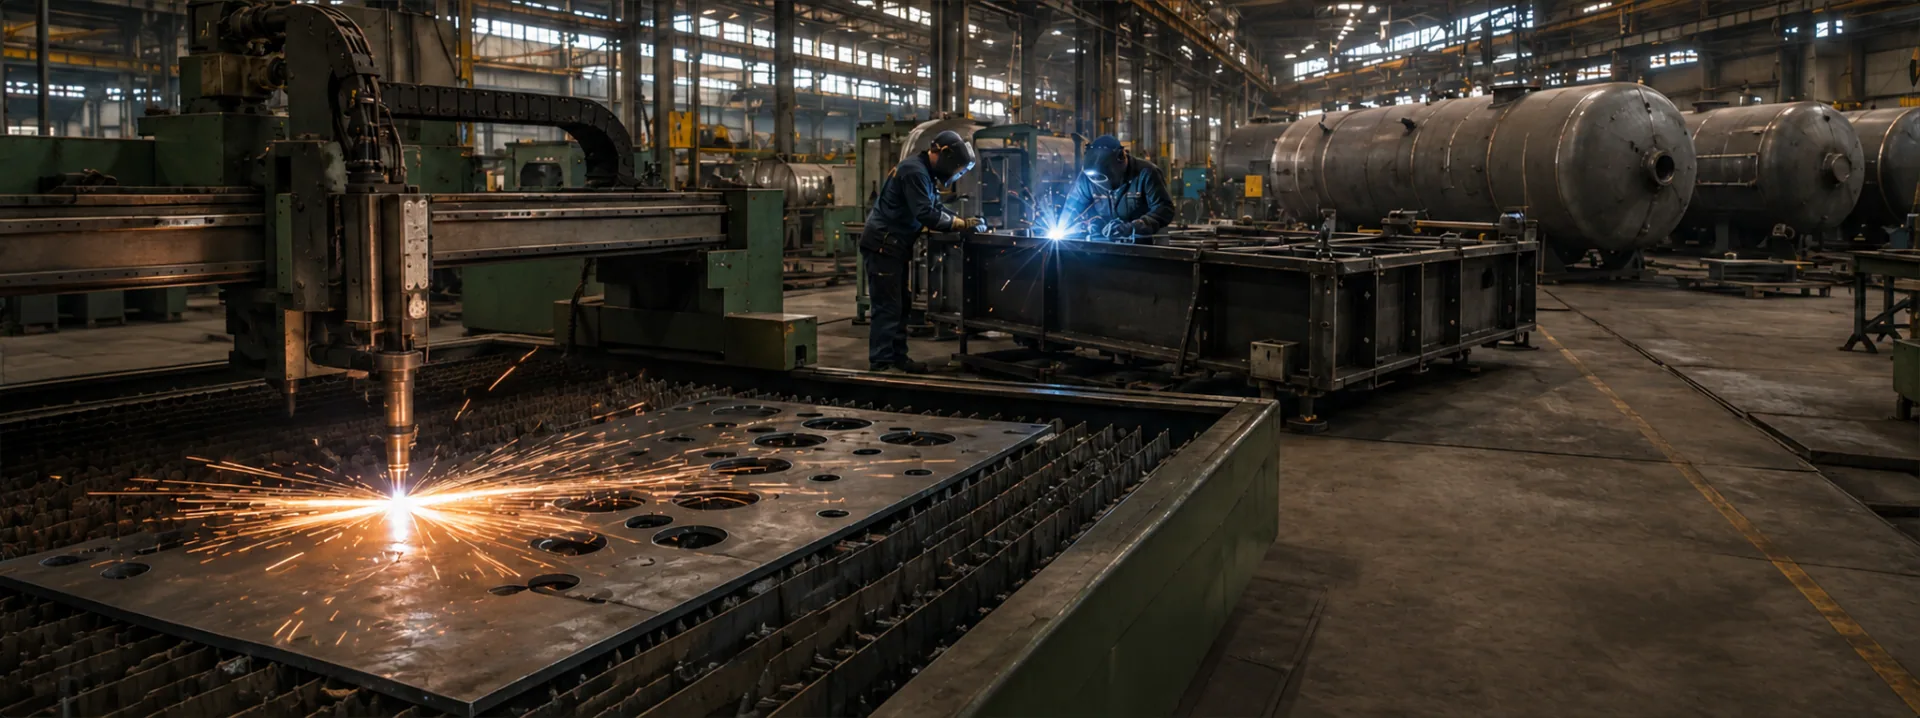
SIVERGUMA production hall

One production process.Multiple technologies.A result defined by the project.

  1. 01

    Welding.

    MIG and MAG welding of steel products with a total weight of up to 10 tonnes.

  2. 02

    Sheet Processing.

    Laser sheet cutting up to 2.5 × 9 m and plasma cutting up to 2.5 × 7 m.

  3. 03

    Tube and Profile Processing.

    Laser cutting of tubes and profiles with lengths of up to 12 m.

  4. 04

    Forming and Finishing.

    Sheet rolling up to 16 mm, bending, shot blasting and powder coating.

Inside SIVERGUMA production

A controlled route
from technical requirements
to the finished product.

Manufacturing is organized as a connected sequence of engineering, processing, assembly, finishing and inspection operations.

The exact route depends on the type of product. A custom component may require several individual metalworking operations, while an industrial tank or engineered field system may pass through the complete production cycle.

Coordination between the stages helps maintain dimensional accuracy, production continuity, traceability and compliance with the approved project documentation.

SIVERGUMA production workshop

Production process / 01–08

Every stage prepares the next one.

01

Requirement and Technical Review

The production process begins with an analysis of the intended application, operating conditions, drawings, specifications, required standards, order volume and delivery requirements.

The team determines technical feasibility, identifies information that requires clarification and prepares the initial production route.

Technical requirements review
02

Engineering and Production Preparation

Technical documentation is reviewed and adapted for manufacturing. Materials, dimensions, tolerances, connections, assembly sequence, welding requirements and control points are defined.

Where required, production drawings, cutting layouts, bills of materials and operation sheets are prepared.

Stage resultDocumentation package released for production.

Engineering documentation preparation
03

Material Reception and Preparation

Steel sheets, profiles, tubes and other components are received, identified and prepared for processing.

Material grade, dimensions, quantity, surface condition and accompanying documentation are checked before the material enters production.

Stage resultVerified and identified materials prepared for processing.

Steel material reception
04

Cutting and Initial Processing

Metal is cut according to the approved production documentation. Depending on the material, geometry and dimensions, the production route may include laser sheet cutting, plasma cutting or laser cutting of tubes and profiles.

Individual parts are marked and prepared for subsequent forming or assembly.

Stage resultCut components corresponding to approved geometry.

Laser metal cutting
05

Forming and Preparation for Assembly

Flat and linear components are formed into the required geometry using rolling and bending operations.

This stage may include sheet rolling for cylindrical tank shells, sheet bending, and bending of tubes and profiles.

The accuracy of critical dimensions is checked before parts are transferred to assembly.

Stage resultFormed components prepared for positioning and assembly.

Metal forming operation
06

Welding and Assembly

Components are positioned, fixed and joined into the final structure. MIG and MAG welding processes are used according to the material, joint type and project requirements.

Assembly may include tank shells, structural supports, frames, technological connections, access elements and additional product-specific components.

Stage resultCompleted welded structure ready for inspection and finishing.

Welding and steel assembly
07

Surface Preparation and Finishing

The completed structure is prepared for the protective or decorative coating specified for the project.

Production capabilities include shot blasting and powder coating. Other coating systems may be selected according to the material, intended application and operating environment.

Stage resultProtected surface corresponding to approved finishing specification.

Protective surface finishing
08

Final Inspection, Documentation and Shipment

The completed product undergoes final visual and dimensional inspection. Project-specific functional, tightness or coating checks are performed where applicable and contractually required.

The product is documented, prepared for safe transportation and transferred for shipment according to the agreed delivery schedule.

Stage resultInspected, documented and packaged product ready for delivery.

Final inspection and shipment

Production equipment

Technology selected for the material and the task.

SIVERGUMA’s equipment covers the key operations required for processing sheet metal, tubes, profiles and welded steel structures.

The combination of cutting, forming, welding and finishing technologies enables the company to manufacture both individual components and complete industrial products.

Equipment manufacturers, model names, power ratings, operating accuracy and commissioning dates must be added after confirmation by the customer.

01

MIG and MAG Welding

Verified capability:

Welding of steel structures and components of different sizes with a total product weight of up to 10 tonnes.

Temporary data required:

  • number of welding stations;
  • supported material grades and thicknesses;
  • welding personnel qualifications;
  • maximum assembly dimensions;
  • available positioning equipment.
MIG and MAG welding station
02

Laser Sheet Cutting

Verified capability:

Laser cutting of sheet metal up to 2.5 metres wide and up to 9 metres long.

Temporary data required:

  • equipment manufacturer and model;
  • laser power;
  • supported steel types;
  • maximum cutting thickness;
  • positioning accuracy;
  • loading and unloading system.
Laser sheet cutting machine
03

Plasma Sheet Cutting

Verified capability:

Plasma cutting of sheet metal up to 2.5 metres wide and up to 7 metres long.

Temporary data required:

  • equipment manufacturer and model;
  • plasma-source power;
  • supported material thickness;
  • cutting accuracy;
  • supported contour complexity;
  • extraction and filtration system.
Plasma sheet cutting machine
04

Tube and Profile Laser Cutting

Verified capability:

Laser cutting of tubes and profiles with different cross-sections and lengths of up to 12 metres.

Temporary data required:

  • supported profile shapes;
  • minimum and maximum cross-section;
  • maximum wall thickness;
  • cutting-head capabilities;
  • positioning accuracy;
  • automatic loading availability.
Tube and profile laser cutting
05

Sheet Rolling

Verified capability:

Rolling of sheet metal up to 16 mm thick and up to 2 metres wide.

Temporary data required:

  • equipment manufacturer and model;
  • number of rolls;
  • minimum rolling diameter;
  • supported steel grades;
  • maximum rolling width for different thicknesses;
  • control-system type.
Sheet rolling machine

Additional equipment and operations

Sheet metal bending

Sheet Metal Cutting and Bending

Preparation and forming of sheet components according to project geometry.

Tube and profile bending

Tube and Profile Bending

Forming of tubes and profiles with different cross-sections.

Shot blasting

Shot Blasting

Mechanical preparation of metal surfaces before coating.

Powder coating

Powder Coating

Application of a durable protective and decorative polymer coating.

Production workshops

Separate production zones.
One connected workflow.

The provisional production structure is divided into functional areas corresponding to the main manufacturing stages.

This organization reduces unnecessary movement of materials, separates operations with different technical and safety requirements and supports control throughout the production route.

01

Material Preparation and Cutting

Reception, storage, identification, layout and cutting of sheets, tubes and profiles.

Operations

  • incoming material inspection;
  • laser sheet cutting;
  • plasma cutting;
  • tube and profile cutting;
  • marking and sorting of parts.
Material preparation and cutting workshop
02

Forming and Component Preparation

Formation of cut parts into the geometry required for subsequent assembly.

Operations

  • sheet rolling;
  • sheet bending;
  • tube and profile bending;
  • edge preparation;
  • preparation of assembly components.
Forming and component preparation workshop
03

Welding and Assembly

Assembly of individual components, steel structures, industrial tanks and engineered systems.

Operations

  • positioning and temporary fixing;
  • MIG and MAG welding;
  • assembly of structural supports;
  • installation of technological connections;
  • intermediate dimensional control.
Welding and assembly workshop
04

Surface Preparation and Coating

Preparation and protection of metal surfaces according to the approved coating specification.

Operations

  • surface cleaning;
  • shot blasting;
  • preparation before coating;
  • powder coating;
  • visual inspection of finished surfaces.
Surface preparation and coating workshop
05

Final Assembly and Inspection

Installation of auxiliary components, final product inspection and preparation of complete supply sets.

Operations

  • final assembly;
  • installation of accessories;
  • functional checks;
  • dimensional and visual inspection;
  • verification of equipment sets;
  • preparation of documentation.
Final assembly and inspection workshop
06

Packaging and Dispatch

Preparation of completed products for storage, loading and transportation.

Operations

  • transport protection;
  • packaging of components and accessories;
  • marking;
  • loading preparation;
  • dispatch-document verification.
Packaging and dispatch zone

Quality control

Quality is checked throughout the process, not only at the end.

Quality control is integrated into the production route through defined inspection points.

The purpose of control is to verify that materials, individual parts, welded assemblies, protective coatings and completed products correspond to the approved technical documentation and contractual requirements.

For oil storage tanks, manufacturing requirements are aligned with EN 12285-1 and EN 12285-2 where applicable.

01

Documentation Review

Verification of drawings, specifications, materials, tolerances, standards and required inspection procedures before production.

Production documentation review
02

Incoming Material Control

Verification of material identification, dimensions, quantity, visible condition and accompanying certificates.

Incoming material control
03

Cutting and Forming Control

Inspection of part geometry, dimensions, cutting quality, bend parameters and formed sections.

Cutting and forming control
04

Welding Control

Monitoring of assembly position, joint preparation, welding sequence and visible weld quality.

Additional non-destructive testing may be performed where required by the project.

Welding quality control
05

Surface and Coating Control

Inspection of surface preparation, coating continuity, appearance and thickness where measurement is required.

Surface and coating control
06

Final Product Control

Final visual and dimensional inspection, configuration verification and functional or tightness testing where applicable.

Final product control
07

Documentation and Release

Confirmation that the required inspection records, technical documents and product equipment are complete before shipment.

Documentation and product release

Documentation and Release

  • incoming material inspection record;
  • material certificates;
  • dimensional inspection report;
  • welding inspection record;
  • non-destructive testing report, where required;
  • functional or tightness test report, where required;
  • coating inspection report;
  • final acceptance checklist;
  • product technical passport;
  • packing and equipment list.

Production media

See the process.
Understand the capability.

The production gallery shows the environment, equipment, operations and people behind SIVERGUMA’s finished products.

The media content should focus on real work: steel entering production, individual operations being performed, structures taking shape, control procedures and completed products prepared for delivery.

SIVERGUMA production hall

Main production film

From material
to field-ready product

A cinematic production film following the complete manufacturing route: technical preparation, cutting, forming, welding, assembly, surface treatment, inspection and shipment.

Panoramic production environment
01

Production Environment.

Wide panoramic views of workshops, production lines and work areas.

Production equipment in operation
02

Equipment in Operation.

Laser cutting, plasma cutting, rolling, bending and welding equipment during real production.

SIVERGUMA production specialists
03

People and Expertise.

Qualified specialists preparing, manufacturing, assembling and inspecting products.

Steel manufacturing detail
04

Manufacturing Details.

Steel surfaces, cut edges, formed sections, welds, connections and coating details.

Production quality control
05

Quality Control.

Measurement, visual inspection, documentation and product acceptance.

Completed SIVERGUMA products
06

Completed Products.

Industrial tanks, steel structures and field systems before loading or deployment.

Manufacturing capacity

Capacity measured
by what can be produced.

SIVERGUMA’s manufacturing capabilities support products of different sizes and levels of complexity—from individual steel components to large welded tanks and project-specific field systems.

The verified parameters below describe the dimensional and technological limits currently represented in the company materials.

Verified capabilities

Swipe for verified parameters

CapabilityVerified parameter
MIG and MAG weldingProducts up to 10 tonnes
Laser sheet cuttingUp to 2.5 × 9 m
Plasma sheet cuttingUp to 2.5 × 7 m
Tube and profile cuttingLengths up to 12 m
Sheet rollingThickness up to 16 mm, width up to 2 m
Additional operationsSheet bending, tube and profile bending, shot blasting, powder coating

Products represented within current capabilities

01

Individual steel components

Individual steel components
02

Welded steel structures

Welded steel structures
03

Aboveground and underground oil storage tanks

Oil storage tank
04

Receiving tanks for drilling operations

Receiving tank for drilling
05

Military and emergency tent frames

Military tent frame
06

Autonomous field shower systems

Autonomous field shower system
07

Solid-fuel field stoves

Solid-fuel field stove
08

Project-specific industrial equipment

Project-specific industrial equipment

Production data to be provided

  • Total production area To be provided
  • Number and area of production workshops To be provided
  • Number of production shifts To be provided
  • Number of employees and certified specialists To be provided
  • Overhead crane and lifting capacity To be provided
  • Maximum overall product dimensions To be provided
  • Monthly steel-processing capacity To be provided
  • Annual production output To be provided
  • Storage and dispatch area To be provided
  • Available transport and loading equipment To be provided

Manufacture with SIVERGUMA

Bring us the requirement.
We will define
the production route.

Tell us what needs to be manufactured, which material and dimensions are required, where the product will be used and which standards, tolerances and delivery conditions must be considered.

The stove operates on all types of solid fuel except coal and provides high-efficiency heating.

Our team will review the available drawings and technical documentation, assess production feasibility and define the operations required to manufacture the product.

SIVERGUMA can provide individual metalworking operations or coordinate the complete route from material preparation to the finished product.

Information required for assessment

  1. 01Product or component name
  2. 02Intended application
  3. 03Drawings and 3D models, if available
  4. 04Material grade
  5. 05Overall dimensions
  1. 06Material thickness
  2. 07Required quantity
  3. 08Dimensional tolerances
  4. 09Welding requirements
  5. 10Surface-treatment requirements
  1. 11Required standards and documentation
  2. 12Delivery destination
  3. 13Required execution period

One operation or the complete manufacturing cycle.

Technical feasibility, production schedule, minimum order quantity, documentation and pricing are agreed individually according to the product and project requirements.